Drilling head
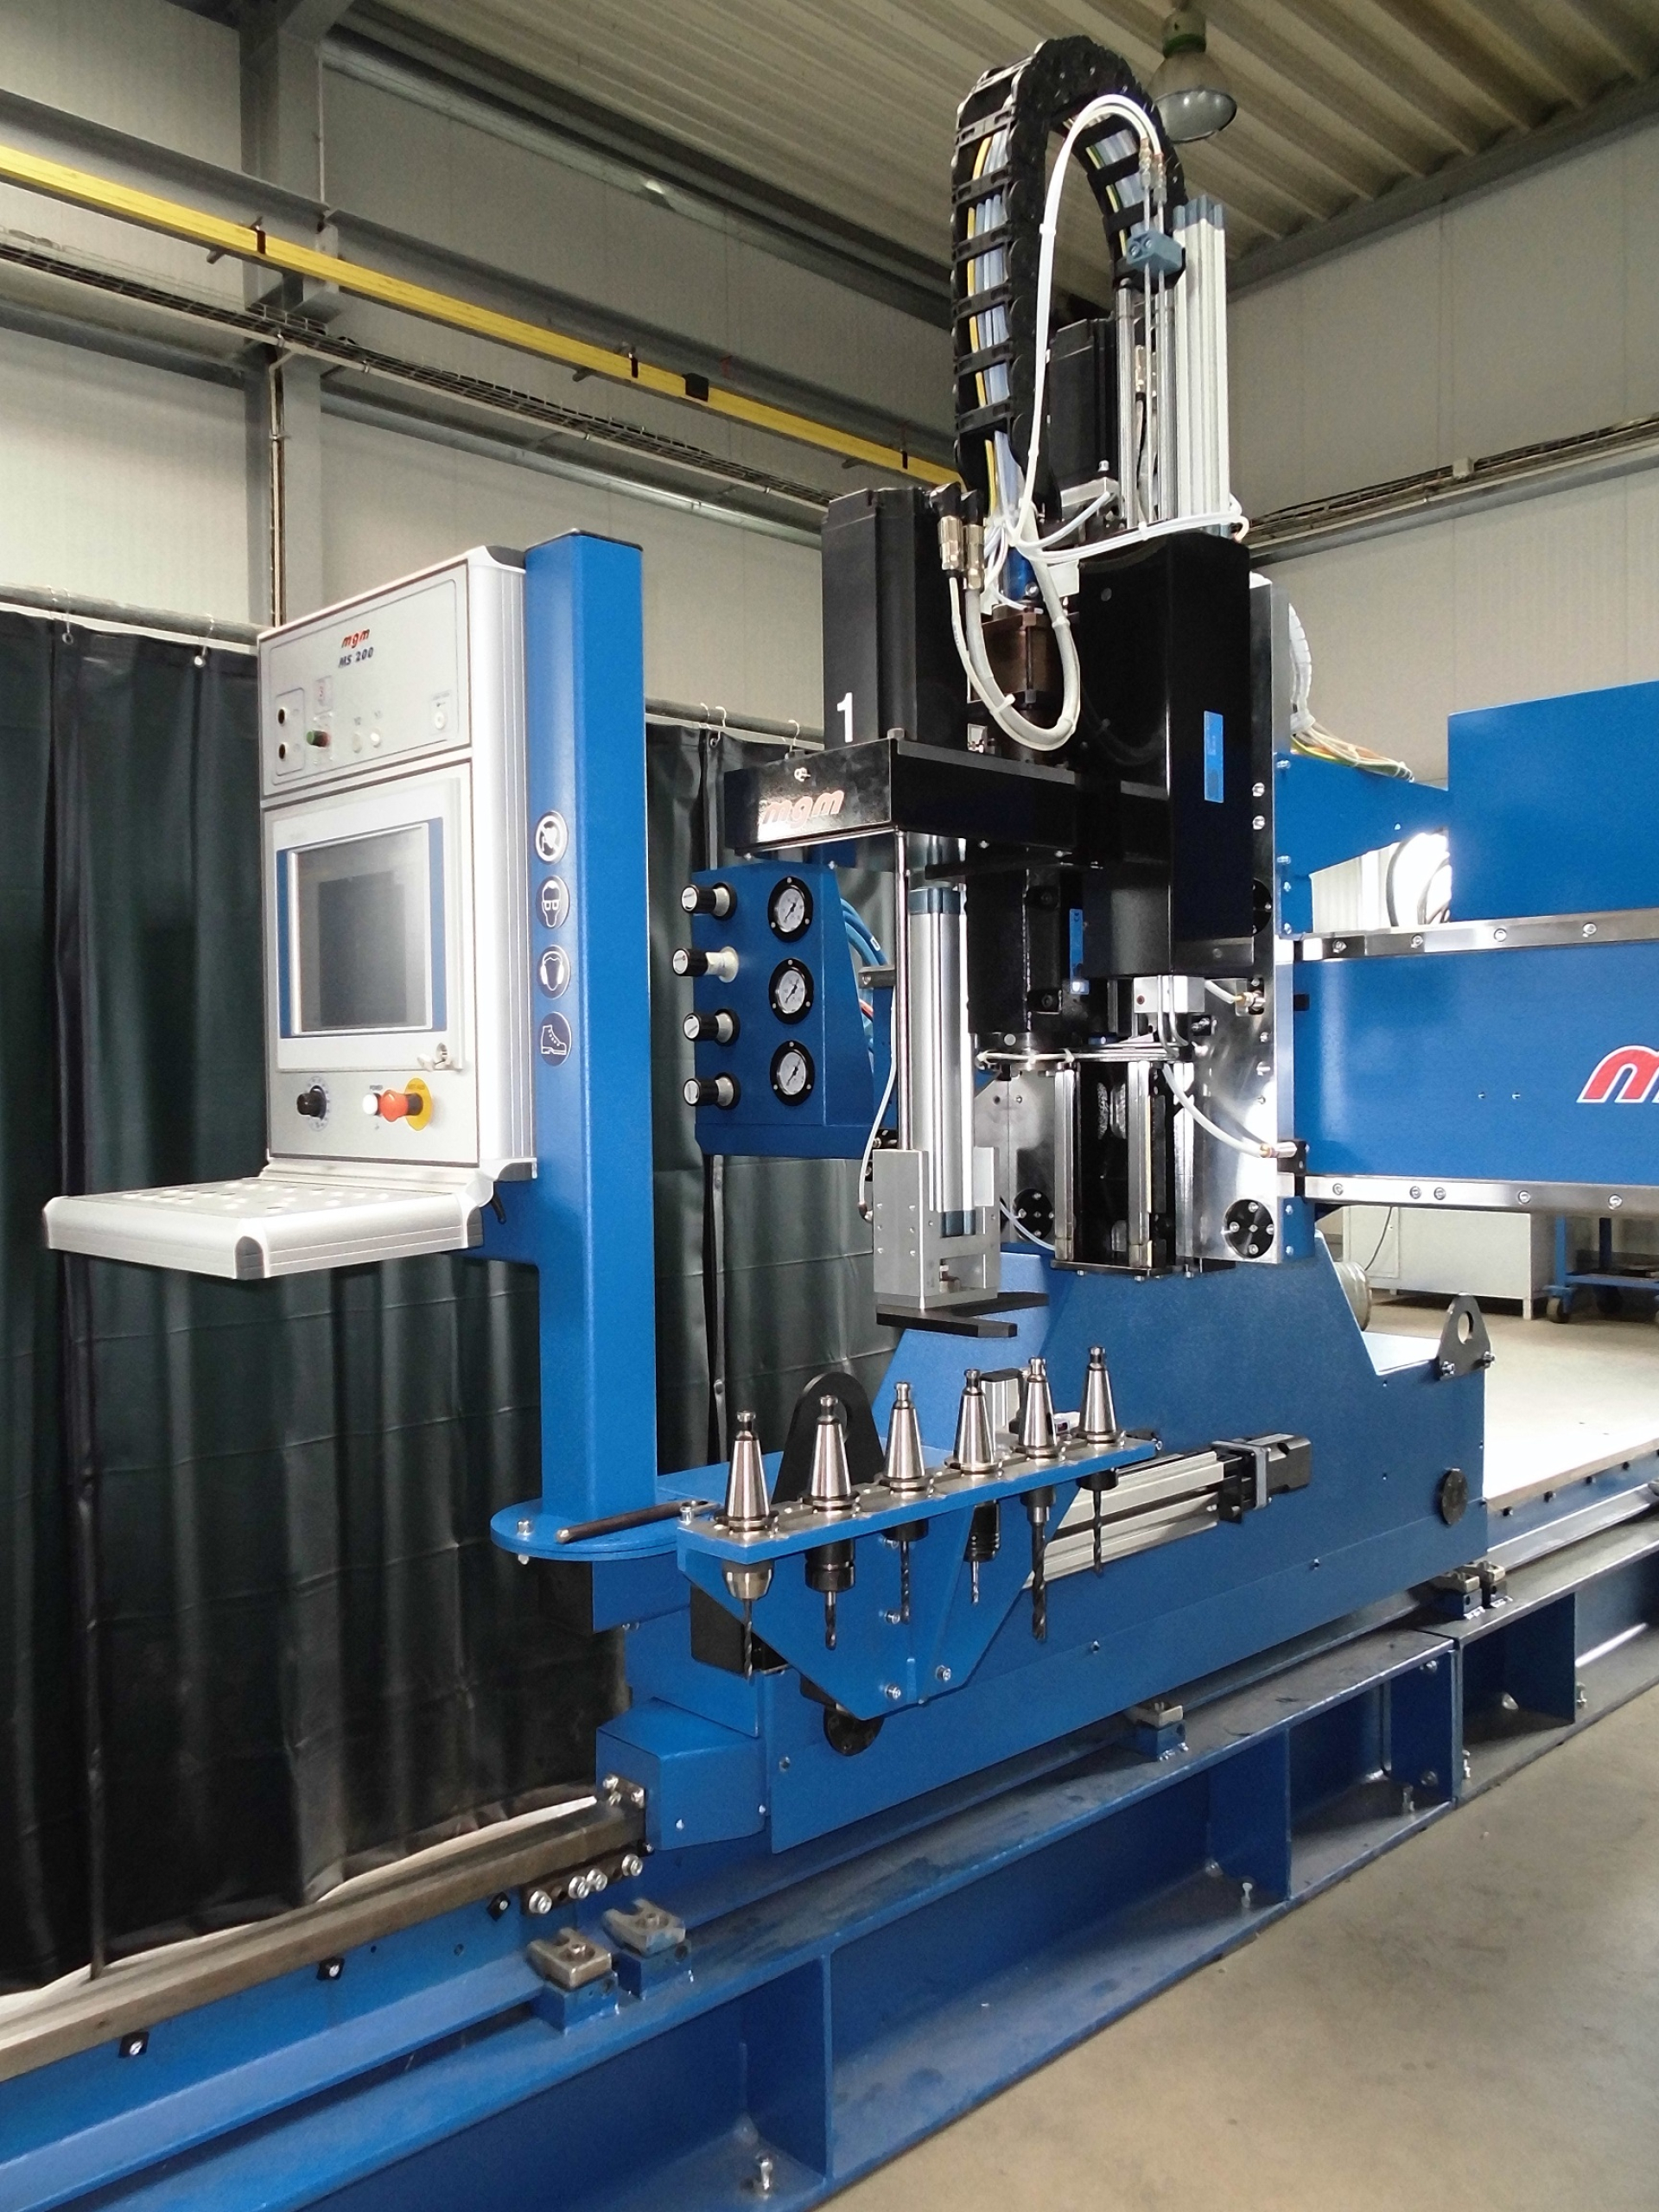
The MAX 40R drilling unit is designed for drilling and also allows for tapping. It is equipped with a spindle with a rigid preloaded bearing and pneumatic tool clamping, which enables automatic tool changes. The unit features a supply of cutting fluid for both external and internal tool lubrication, controlled by a solenoid valve, as well as micro-lubrication via an oil mist.
The device includes an automatically controlled stroke feed module, automatic tool length measurement, and an electronically positioned sheet position sensing system at the table clamping. For stability during drilling, a pneumatic sheet hold-down with adjustable travel height is used. The unit is further equipped with a magazine for six tools with automatic tool change, and operation is carried out directly via the CNC control, which also utilizes a tool database for drilling and tapping.
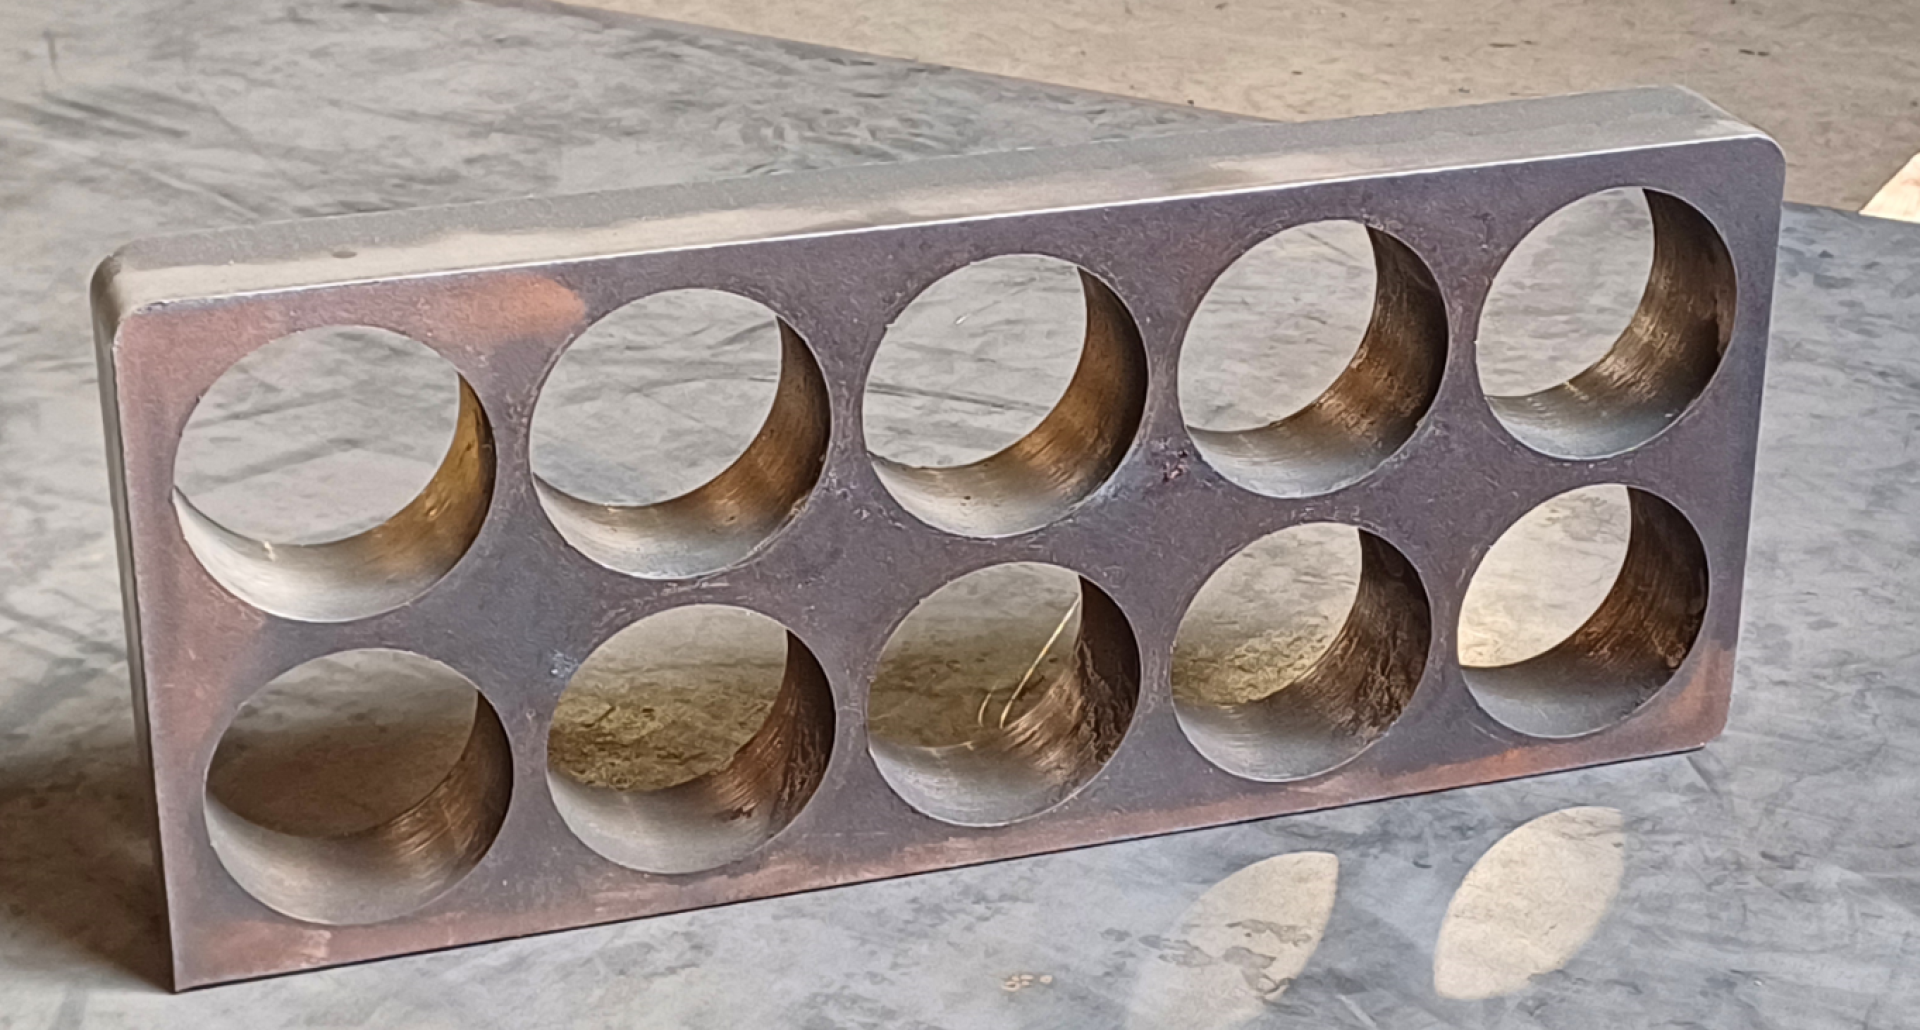
On Omnicut-type machines equipped with a drilling unit, it is possible to create accurate large-diameter holes while minimizing the heat-affected zone. The basic principle is to cut a circular opening with allowance using plasma and then drill it with a drilling head. This method not only removes the heat-affected area but also ensures high hole accuracy in both diameter and roundness. By selecting the appropriate feed rate, low surface roughness can also be achieved.
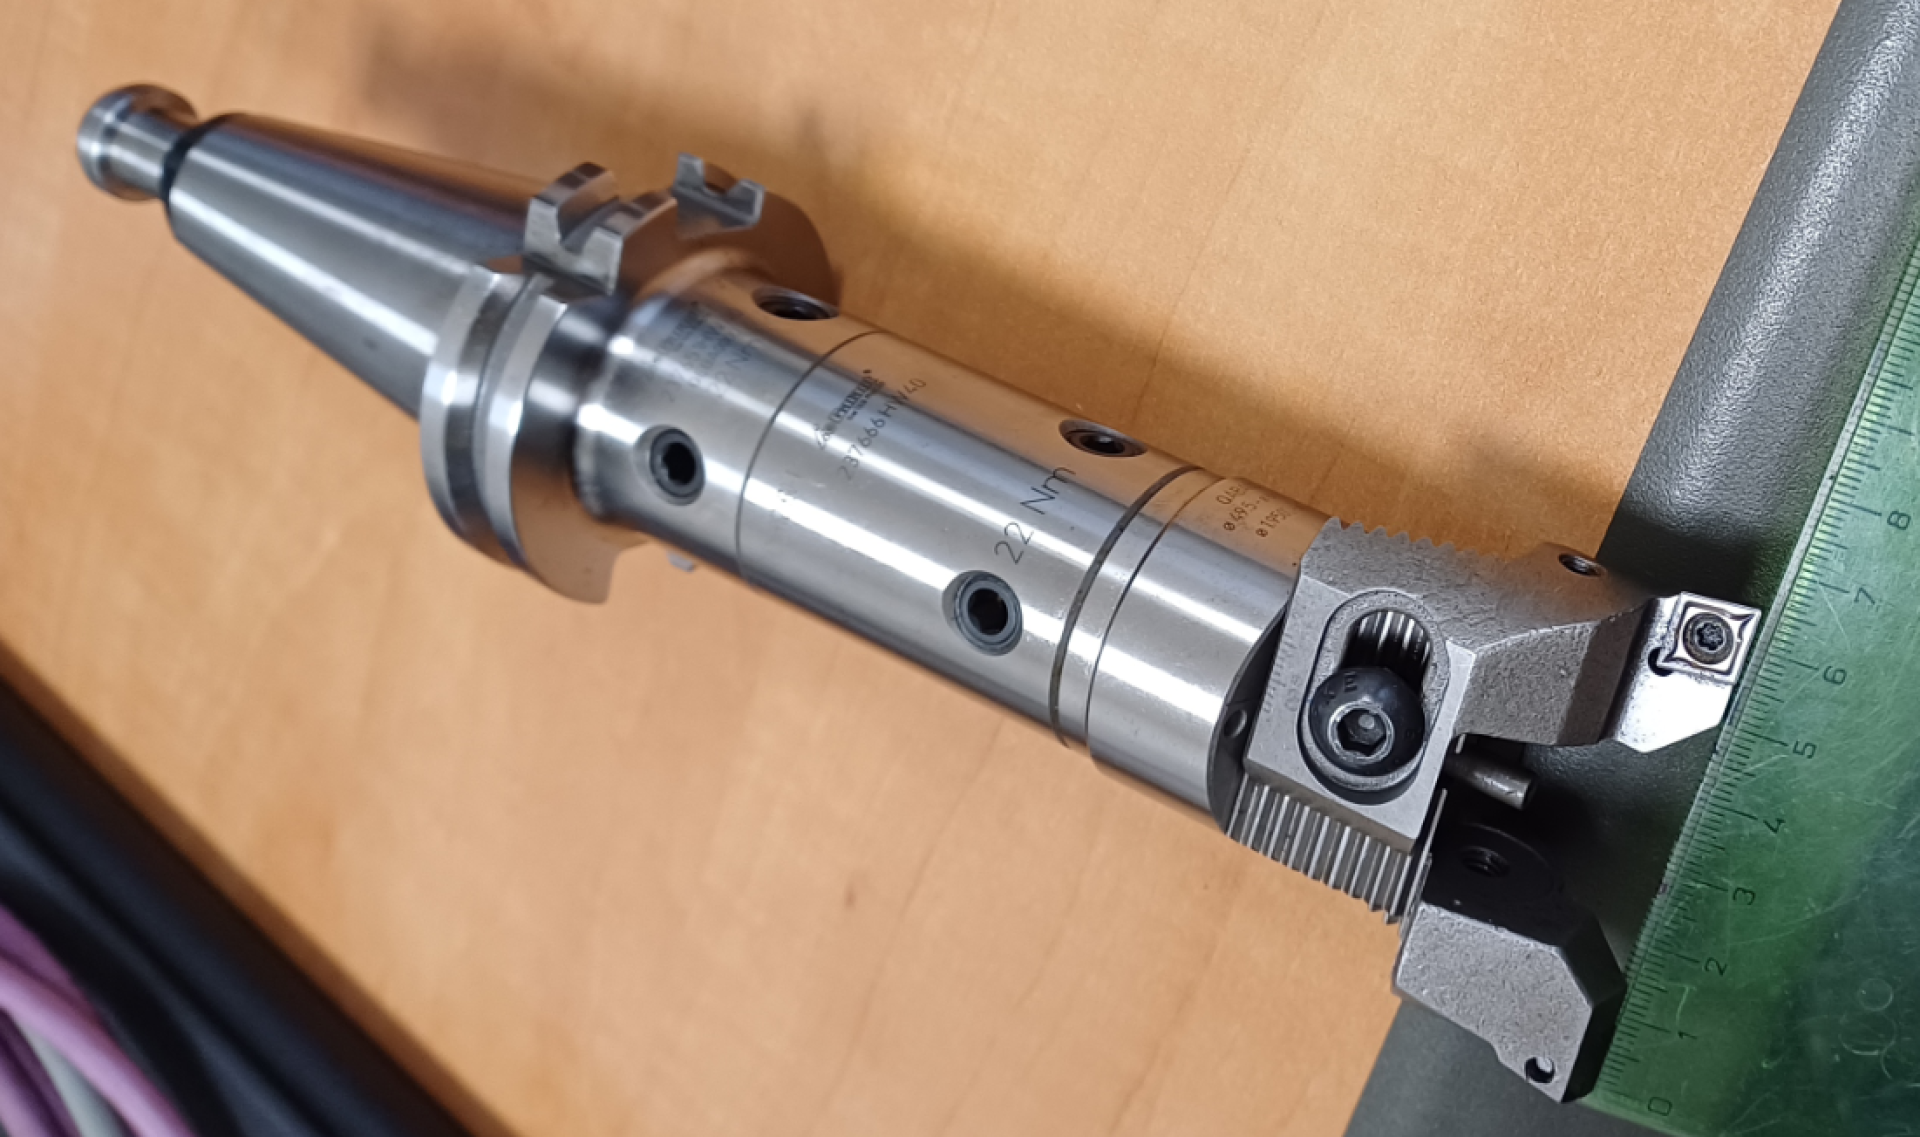
The boring head can be adjusted to different diameters, and the appropriate range is selected according to the required hole size. For example, the boring head we tested has a diameter range of 49.5 to 66.5 mm.
Programming
New programming strategy for SAPSproW
We currently have a new drilling strategy aimed at significantly simplifying the entire process.
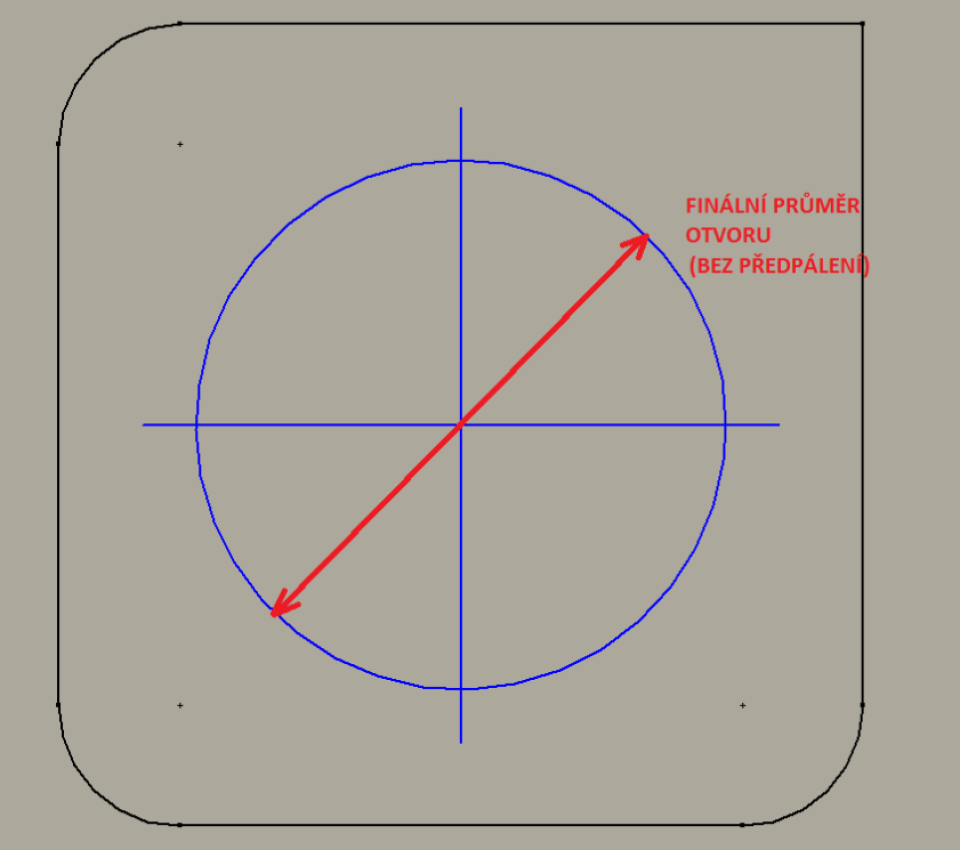
Example of drilling
Material | S235JR |
Thickness: | 40 mm |
Diameter: | 66 mm |
Spindle speed: | 500 ot/min |
Feed: | 0,14 mm/ot |
Cooling/Lubrication: | Yes – external |